Industrial Epoxy Flooring: Built for Strength, Engineered for Longevity
Industrial Epoxy Flooring: Built for Strength, Engineered for Longevity
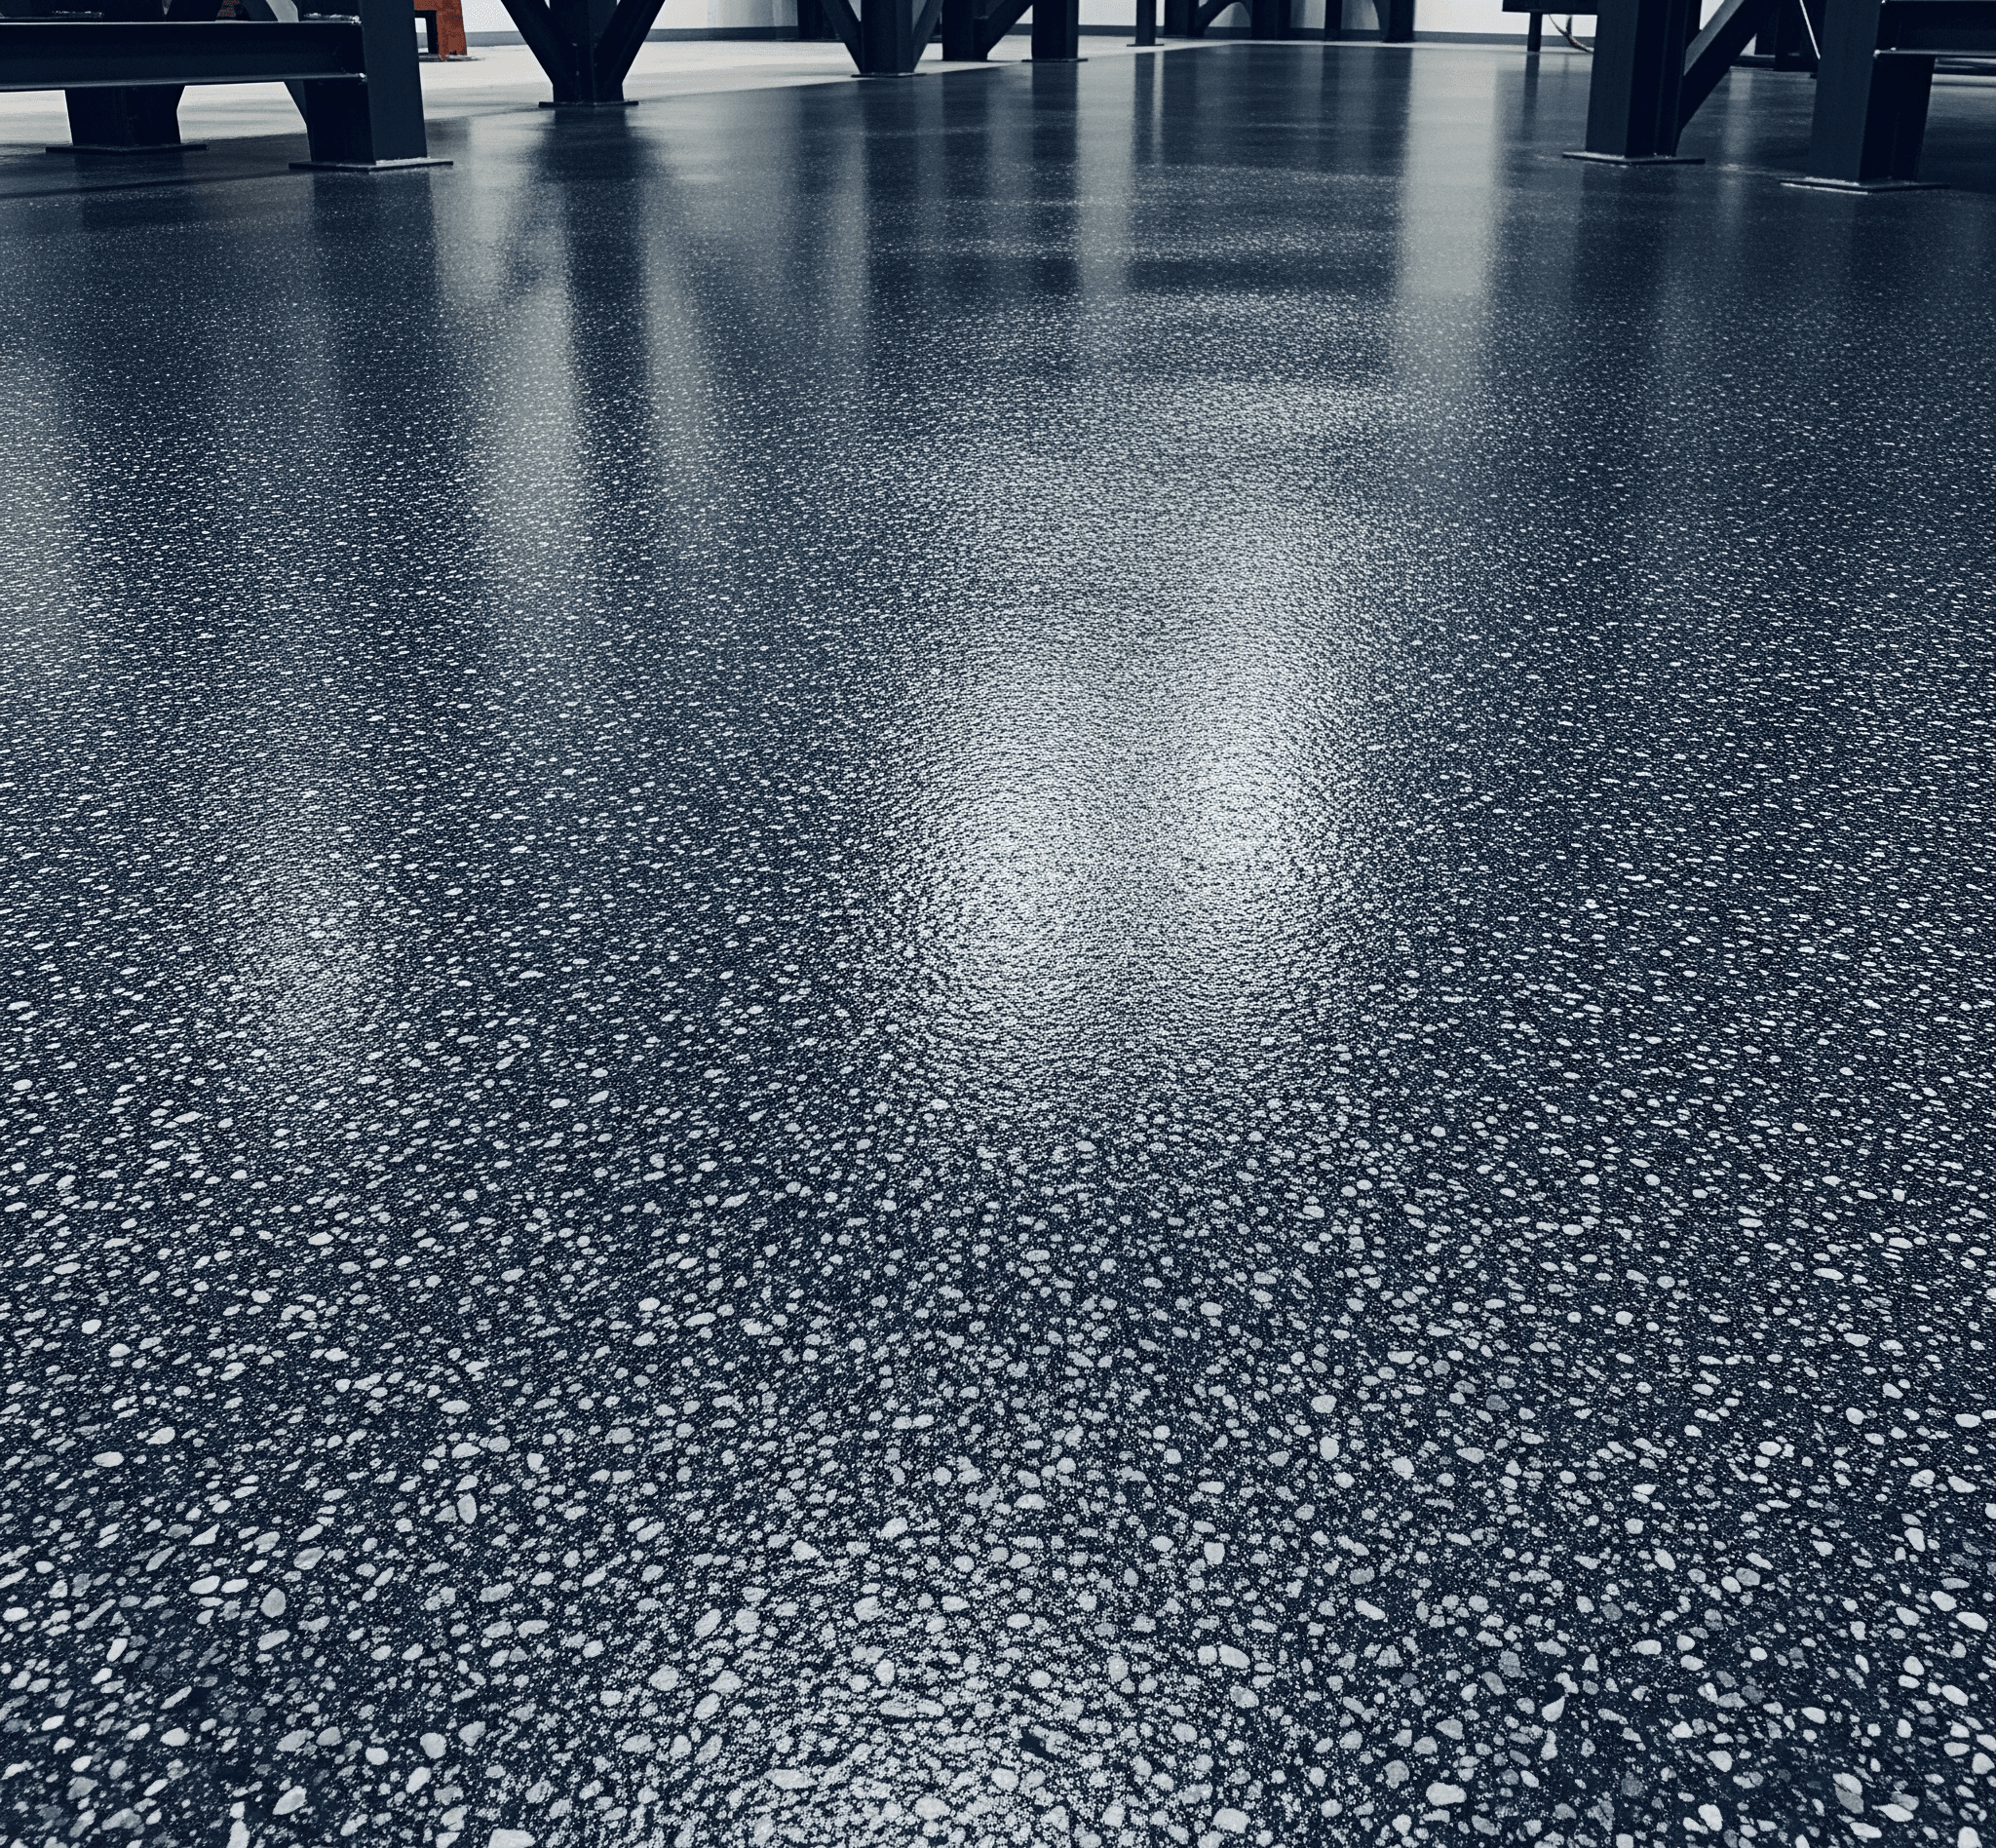
Industrial environments call for flooring solutions that can endure the intense pressure of daily operations. The surface must support everything from foot traffic and machinery to chemical exposure and shifting temperatures. In these demanding spaces, a standard floor won’t cut it—your facility needs a floor that performs consistently under pressure. Whether you manage a warehouse, factory, or manufacturing plant, industrial epoxy flooring offers unmatched resilience, safety, and efficiency. These facilities often face constant pressure from equipment movement, chemical exposure, and foot traffic, all of which can lead to premature wear and unsafe conditions. Epoxy flooring delivers an integrated solution—reinforcing the structure, simplifying maintenance, and creating a safer, more productive environment for workers and machinery alike.
At Los Angeles Epoxy, we deliver high-performance solutions tailored to meet the demands of your operations. From food-grade environments to heavy-load manufacturing, our coatings are designed to withstand impact, abrasion, chemical spills, and extreme temperature changes—without compromise.
Why Industrial Epoxy Flooring is the Smart Choice
Most concrete floors in industrial spaces wear down fast. Forklifts, foot traffic, dropped tools, and chemical exposure—all contribute to surface damage, dust, and safety hazards. That’s where epoxy industrial flooring comes in.
High Load Resistance: Supports heavy equipment and machinery.
Chemical Protection: Resists acids, solvents, oils, and cleaners.
Slip Resistance: Optional textured coatings for worker safety.
Low Maintenance: No waxing, stripping, or resealing needed.
Cost Efficiency: Lasts up to 20 years with minimal upkeep.
This isn’t just about aesthetics—it’s about protecting productivity, reducing downtime, and maintaining regulatory compliance.
In addition to these core benefits, epoxy flooring also provides an aesthetic upgrade to your industrial space. With customizable colors and finishes, you can align the flooring with your company branding or safety zone guidelines. The seamless finish reduces tripping hazards and makes cleaning effortless, ensuring a safer, more organized workspace. Moreover, by protecting the underlying concrete from cracking or absorbing harmful chemicals, epoxy helps preserve your facility’s structural integrity.
Industrial Epoxy vs. Other Flooring Options
Choosing the right floor for industrial operations means balancing cost, performance, and safety—without sacrificing compliance or functionality. Industrial facilities face demanding conditions that typical flooring options often can’t handle. From chemical spills and forklift traffic to abrasive cleaning and fluctuating temperatures, every square inch of your workspace needs to be reinforced. That’s why understanding how different flooring types compare is essential. Here’s how industrial epoxy flooring stands up against common alternatives:
Feature | Industrial Epoxy Flooring | Concrete Only | Vinyl or Tile |
Load Resistance | Very High | Medium | Low |
Chemical Resistance | Excellent | Low | Moderate |
Durability (Years) | 10–20+ | 3–7 | 3–5 |
Seamless Surface | Yes | No | No |
Cleaning & Maintenance | Very Low | High | Moderate |
Installation Downtime | 2–4 days | N/A | 3–6 days |
Industrial epoxy doesn’t just protect floors—it protects operations.
What Makes Our System Different?
We work with top-tier industrial epoxy resin flooring formulations that exceed industry standards. Our process includes:
Surface Grinding & Prep: Ensures strong adhesion.
Moisture & Vapor Testing: Prevents bubbling and failure.
Primer Application: Bonds resin to concrete.
Epoxy Resin Installation: Can include anti-slip aggregates.
Topcoat Layer: UV protection, gloss, or matte finish.
As trusted industrial epoxy flooring contractors, we coordinate installs around your schedule to minimize disruption. Whether it’s a new facility or a retrofit, we deliver dependable, long-term solutions.
Our system stands out because we don’t take shortcuts. Every stage—from initial site evaluation to post-installation inspection—is executed with precision. We use only commercial-grade epoxy materials that are tested for industrial-grade performance. Plus, we educate our clients about upkeep, ensuring they maximize the lifespan of their flooring. Our experienced crew is trained to handle complex projects, ensuring your flooring investment delivers returns for decades.
Best Applications for Industrial Flooring Epoxy Coating
From light-duty manufacturing to chemical-intensive labs, industrial flooring epoxy coating adapts to virtually any application:
- Warehouses & Distribution Centers
- Food & Beverage Facilities
- Pharmaceutical Plants
- Automotive Assembly Lines
- Electronics Manufacturing
- Cold Storage Rooms
With epoxy flooring industrial systems, each installation is tailored to your workflow and safety requirements.
In each of these settings, epoxy flooring enhances not only durability but also compliance with industry standards. For example, pharmaceutical environments benefit from dust-resistant, easy-to-clean surfaces, while food production areas rely on epoxy’s ability to withstand sanitizing chemicals. Cold storage rooms appreciate their thermal shock resistance, which prevents cracking under fluctuating temperatures. Our team will always recommend the right formulation for your facility’s unique operational demands.
Benefits of Industrial Epoxy Resin Flooring
Impact Resistance: Protects concrete against dropped tools and rolling equipment.
Hygienic: Seamless surfaces prevent bacterial growth and are easy to sanitize.
Customizable: Choose from colors, textures, and performance additives.
Eco-Conscious: Low-VOC options available.
Compliance: Meets OSHA and USDA flooring guidelines.
Epoxy flooring also reduces operational hazards by enhancing visibility and safety. By using color-coded floor zones or reflective coatings, workers can navigate more effectively and avoid dangerous areas. Plus, epoxy’s resistance to water and stains eliminates mold or mildew buildup, which is crucial for facilities focused on health or food safety. Its non-porous surface ensures that no liquids seep through and compromise the integrity of the floor or the products handled in the facility.
FAQs About Industrial Epoxy Flooring
Q1: How long does industrial epoxy flooring last?
With proper installation and regular cleaning, it lasts 10–20 years. To maintain its durability, epoxy floors should be swept or vacuumed daily to remove debris and dirt that can cause scratches. Weekly mopping with a pH-neutral cleaner is also recommended to preserve the gloss and prevent residue buildup. Avoid harsh chemical cleaners, and instead opt for soft-bristle brushes or microfiber mops for best results. Recoating top layers every 5–7 years can help extend lifespan even further. Environmental conditions, traffic load, and chemical exposure will also influence longevity. Choosing professional installation ensures maximum durability and performance.
Q2: How does epoxy compare to polished concrete?
Epoxy provides better chemical resistance and customization. Polished concrete is great for dust control, but doesn’t offer the same level of protection. Epoxy can be textured for slip resistance and layered with performance coatings. It also creates a seamless barrier that prevents moisture penetration and supports hygiene compliance.
Q3: Is epoxy flooring safe for food-grade facilities?
Yes. We offer USDA-compliant, antimicrobial epoxy coatings for food processing and packaging environments. These systems are designed to resist microbial growth and withstand aggressive cleaning procedures. Seamless epoxy eliminates grout lines or gaps where contaminants can accumulate.
Q4: Can you install epoxy in cold or humid areas?
Absolutely. We use moisture-tolerant primers and temperature-controlled curing methods to ensure strong bonding even in challenging environments. Our formulations are selected to withstand variable site conditions without compromising performance. Cold storage, refrigerated zones, and high-humidity facilities benefit greatly from epoxy’s flexibility.
Q5: How long does installation take?
Most projects are completed in 2–4 days, depending on surface condition, square footage, and curing time. We also factor in project coordination to minimize operational disruption. Our team communicates clearly to ensure seamless scheduling, safe workspace practices, and timely completion.
Final Thoughts: Reinforce Your Facility from the Ground Up
Durability isn’t optional in industrial environments—it’s essential for ensuring operational continuity and worker safety. In manufacturing plants, floors must resist constant impact from heavy tools and forklifts. In pharmaceutical and food processing facilities, the surface must endure harsh cleaning chemicals without degrading. And in automotive or chemical plants, chemical spills and thermal stress demand a flooring system that won’t crack or delaminate. Without durable flooring, facilities risk costly repairs, safety violations, and production delays. With industrial epoxy flooring from Los Angeles Epoxy, you’re choosing performance, safety, and long-term value. Whether you operate a food plant, warehouse, or chemical lab, we’ll install a floor that works as hard as you do.
Industrial epoxy flooring not only reduces the risk of workplace injuries but also improves operational efficiency by minimizing floor maintenance downtime. It enhances the professional appearance of your facility, helping you project cleanliness and reliability to clients, partners, and inspectors alike. When safety, compliance, and presentation all align, your business stands out for the right reasons.
Our team provides tailored recommendations based on your industry requirements, space conditions, and future needs. We don’t just install floors—we help future-proof your operation.
Protect & Enhance Your Floors – Contact Us for a Quote!